
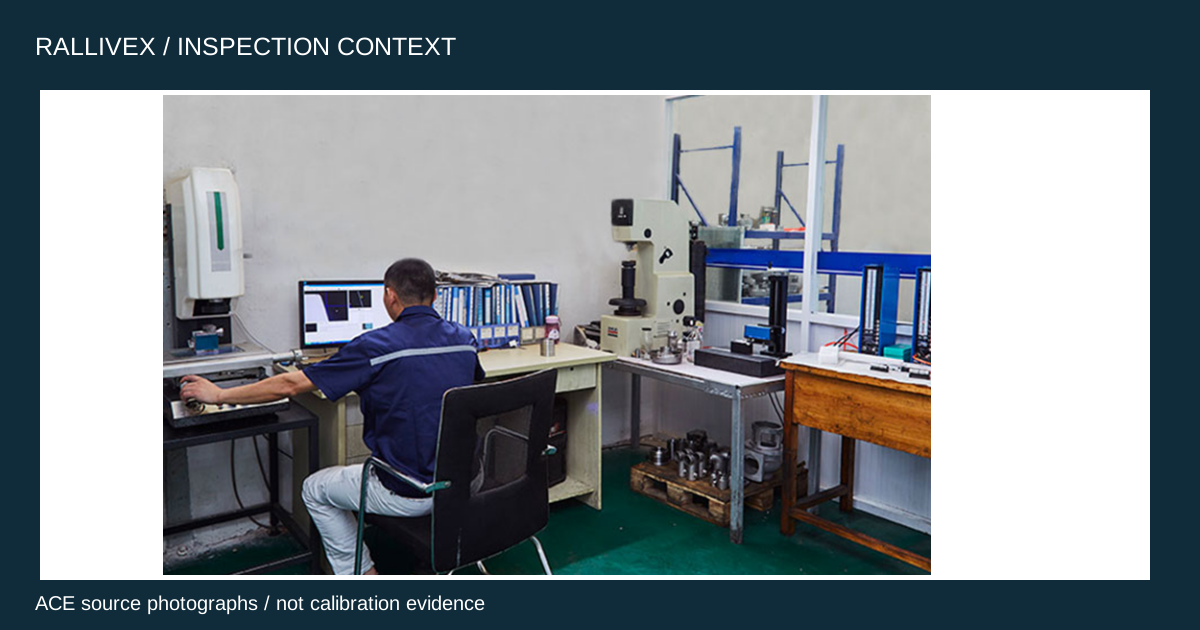
What should you do with a reading close to the limit?
Agree on the acceptance rule before inspection. When a CNC measurement sits near a tolerance limit, the measured value and the inspection method's uncertainty both matter. Two teams can read the same number and reach different decisions if one compares the reading directly with the drawing and the other applies a guard band.
A guard band is the distance between a specification limit and an acceptance limit. Moving the acceptance limit inward can reduce the risk of accepting a nonconforming part, while increasing the chance that a conforming part will require review or fail the chosen acceptance rule. The appropriate trade-off depends on the feature and the agreed inspection plan.
1. Define exactly what each team will measure
For a bore, state whether the requirement is evaluated at specified cross-sections or over a defined portion of the feature. Confirm how the size is evaluated, which locations are sampled and what part condition applies. If the drawing also controls form, identify the separate evidence needed for that requirement.
Ask for the estimated uncertainty for this measurement task. Instrument resolution is one input. A calibration result alone does not describe the effects of the setup, part temperature, operator or sampling strategy. The buyer and supplier should be able to reproduce the comparison from the agreed method.
2. Compare the drawing limit with the acceptance limit
Suppose a machined bore is specified from 20.000 to 20.020 mm. For illustration, assume an expanded uncertainty of 0.003 mm and an agreed rule that requires the entire reported value plus or minus that uncertainty to lie within the specification. The resulting acceptance interval is 20.003 to 20.017 mm, inclusive.
A reading of 20.018 mm is within the drawing limits. Under this illustrative rule, it cannot be declared conforming because its interval extends to 20.021 mm. That result triggers the agreed review path. It does not by itself demonstrate that the physical bore is oversized.
A reading of 20.016 mm gives an interval of 20.013 to 20.019 mm and meets this example rule. Both results concern the same feature and tolerance. The difference is the remaining margin at the nearest limit. The figures are hypothetical and do not describe a company capability.

3. Resolve disagreement before releasing parts
If the supplier and buyer reach different decisions, compare the part identifiers and drawing revisions first. Then compare the measurement locations, evaluation methods, temperature conditions and actual readings. A difference in the definition of the feature can persist even when both instruments are calibrated.
Keep the original result and record why any repeat measurement was needed. Where the initial method cannot support the agreed decision, the teams can agree on an appropriate method with lower uncertainty or refer the result for engineering disposition. Repeating the same setup until a favourable number appears does not resolve the underlying disagreement.
4. Put the rule into the inspection request
For a critical feature, send the tolerance, feature definition, inspection state and decision rule together. Agree who handles a borderline result and whether parts remain on hold pending review.
- Feature: drawing revision, tolerance and evaluation location.
- Method: part condition, setup and measurement uncertainty.
- Decision: acceptance rule, evidence to report and escalation owner.
Ask the report to identify the part or lot, method, unrounded result where available, uncertainty information relevant to the decision, rule applied and disposition. If the requirement is still open, flag it during quotation so it can be reviewed with the quality requirements before order release.
Frequently asked questions
Does a calibrated gauge settle a borderline result?
Calibration contributes evidence about the instrument. The full measurement method and the agreed decision rule still determine how the reported result is used.
Can we add a guard band after seeing the results?
Resolve any missing rule with the buyer and supplier and document the agreement before disposition. Applying a new rule after seeing the data can change the meaning of the original result.
Is a borderline result automatically a rejected part?
Follow the agreed rule. A hold for further evaluation is a possible disposition when the evidence is insufficient for a conformity statement.